AT A GLANCE
- Subject: Why chemical quality and purity influence pharmaceutical manufacturing, formulation, and quality-control testing
- Why it matters to buyers: Stated assay alone does not define suitability — impurity profile, grade, documentation, and consistency all affect whether a chemical fits the process
- Primary areas: Raw-material qualification, formulation consistency, process performance, and QC laboratory testing
- What to request from a supplier: Certificate of Analysis, Safety Data Sheet, product specification, lot traceability, and regulatory documentation
Pharmaceutical manufacturing requires a high level of consistency, precision, and quality control. From active pharmaceutical ingredients and excipients to processing chemicals and laboratory reagents, the quality of every chemical used in production can influence manufacturing performance and finished-product quality. Chemical purity is particularly important because unwanted impurities can affect stability, formulation characteristics, analytical results, and overall product consistency — which is why manufacturers carefully evaluate specifications, grades, impurity profiles, documentation, and supplier reliability before approving a raw material.
Why Chemical Quality Matters in Pharmaceutical Manufacturing
Pharmaceutical products must meet carefully defined quality requirements, so the raw materials used during manufacturing need to be consistent and appropriate for their intended applications. Chemical quality can affect product consistency, manufacturing performance, formulation stability, analytical testing, impurity control, batch-to-batch reproducibility, regulatory compliance, and ultimately patient safety. In the United States, these expectations are formalized through FDA Current Good Manufacturing Practice (CGMP) regulations, which address the control of components and raw materials used in drug manufacturing. A chemical may appear suitable based on its name and stated assay, but its complete specification can contain important information about trace impurities, moisture, residual solvents, metals, and other characteristics. This is why pharmaceutical manufacturers evaluate more than simply the percentage purity of a chemical.
What Does Chemical Purity Mean?
Chemical purity generally refers to the proportion of the desired substance present in a material compared with unwanted substances or impurities. A chemical described as having a high assay value may contain only a small proportion of other substances, but the identity and concentration of those impurities can still be important. Depending on the application, manufacturers may need to evaluate assay, organic and inorganic impurities, trace metals, water content, residual solvents, related substances, microbiological characteristics, and physical properties. The acceptable limits depend on the specific chemical and its intended pharmaceutical application, and are often informed by ICH quality guidelines covering organic impurities, residual solvents, and elemental impurities.
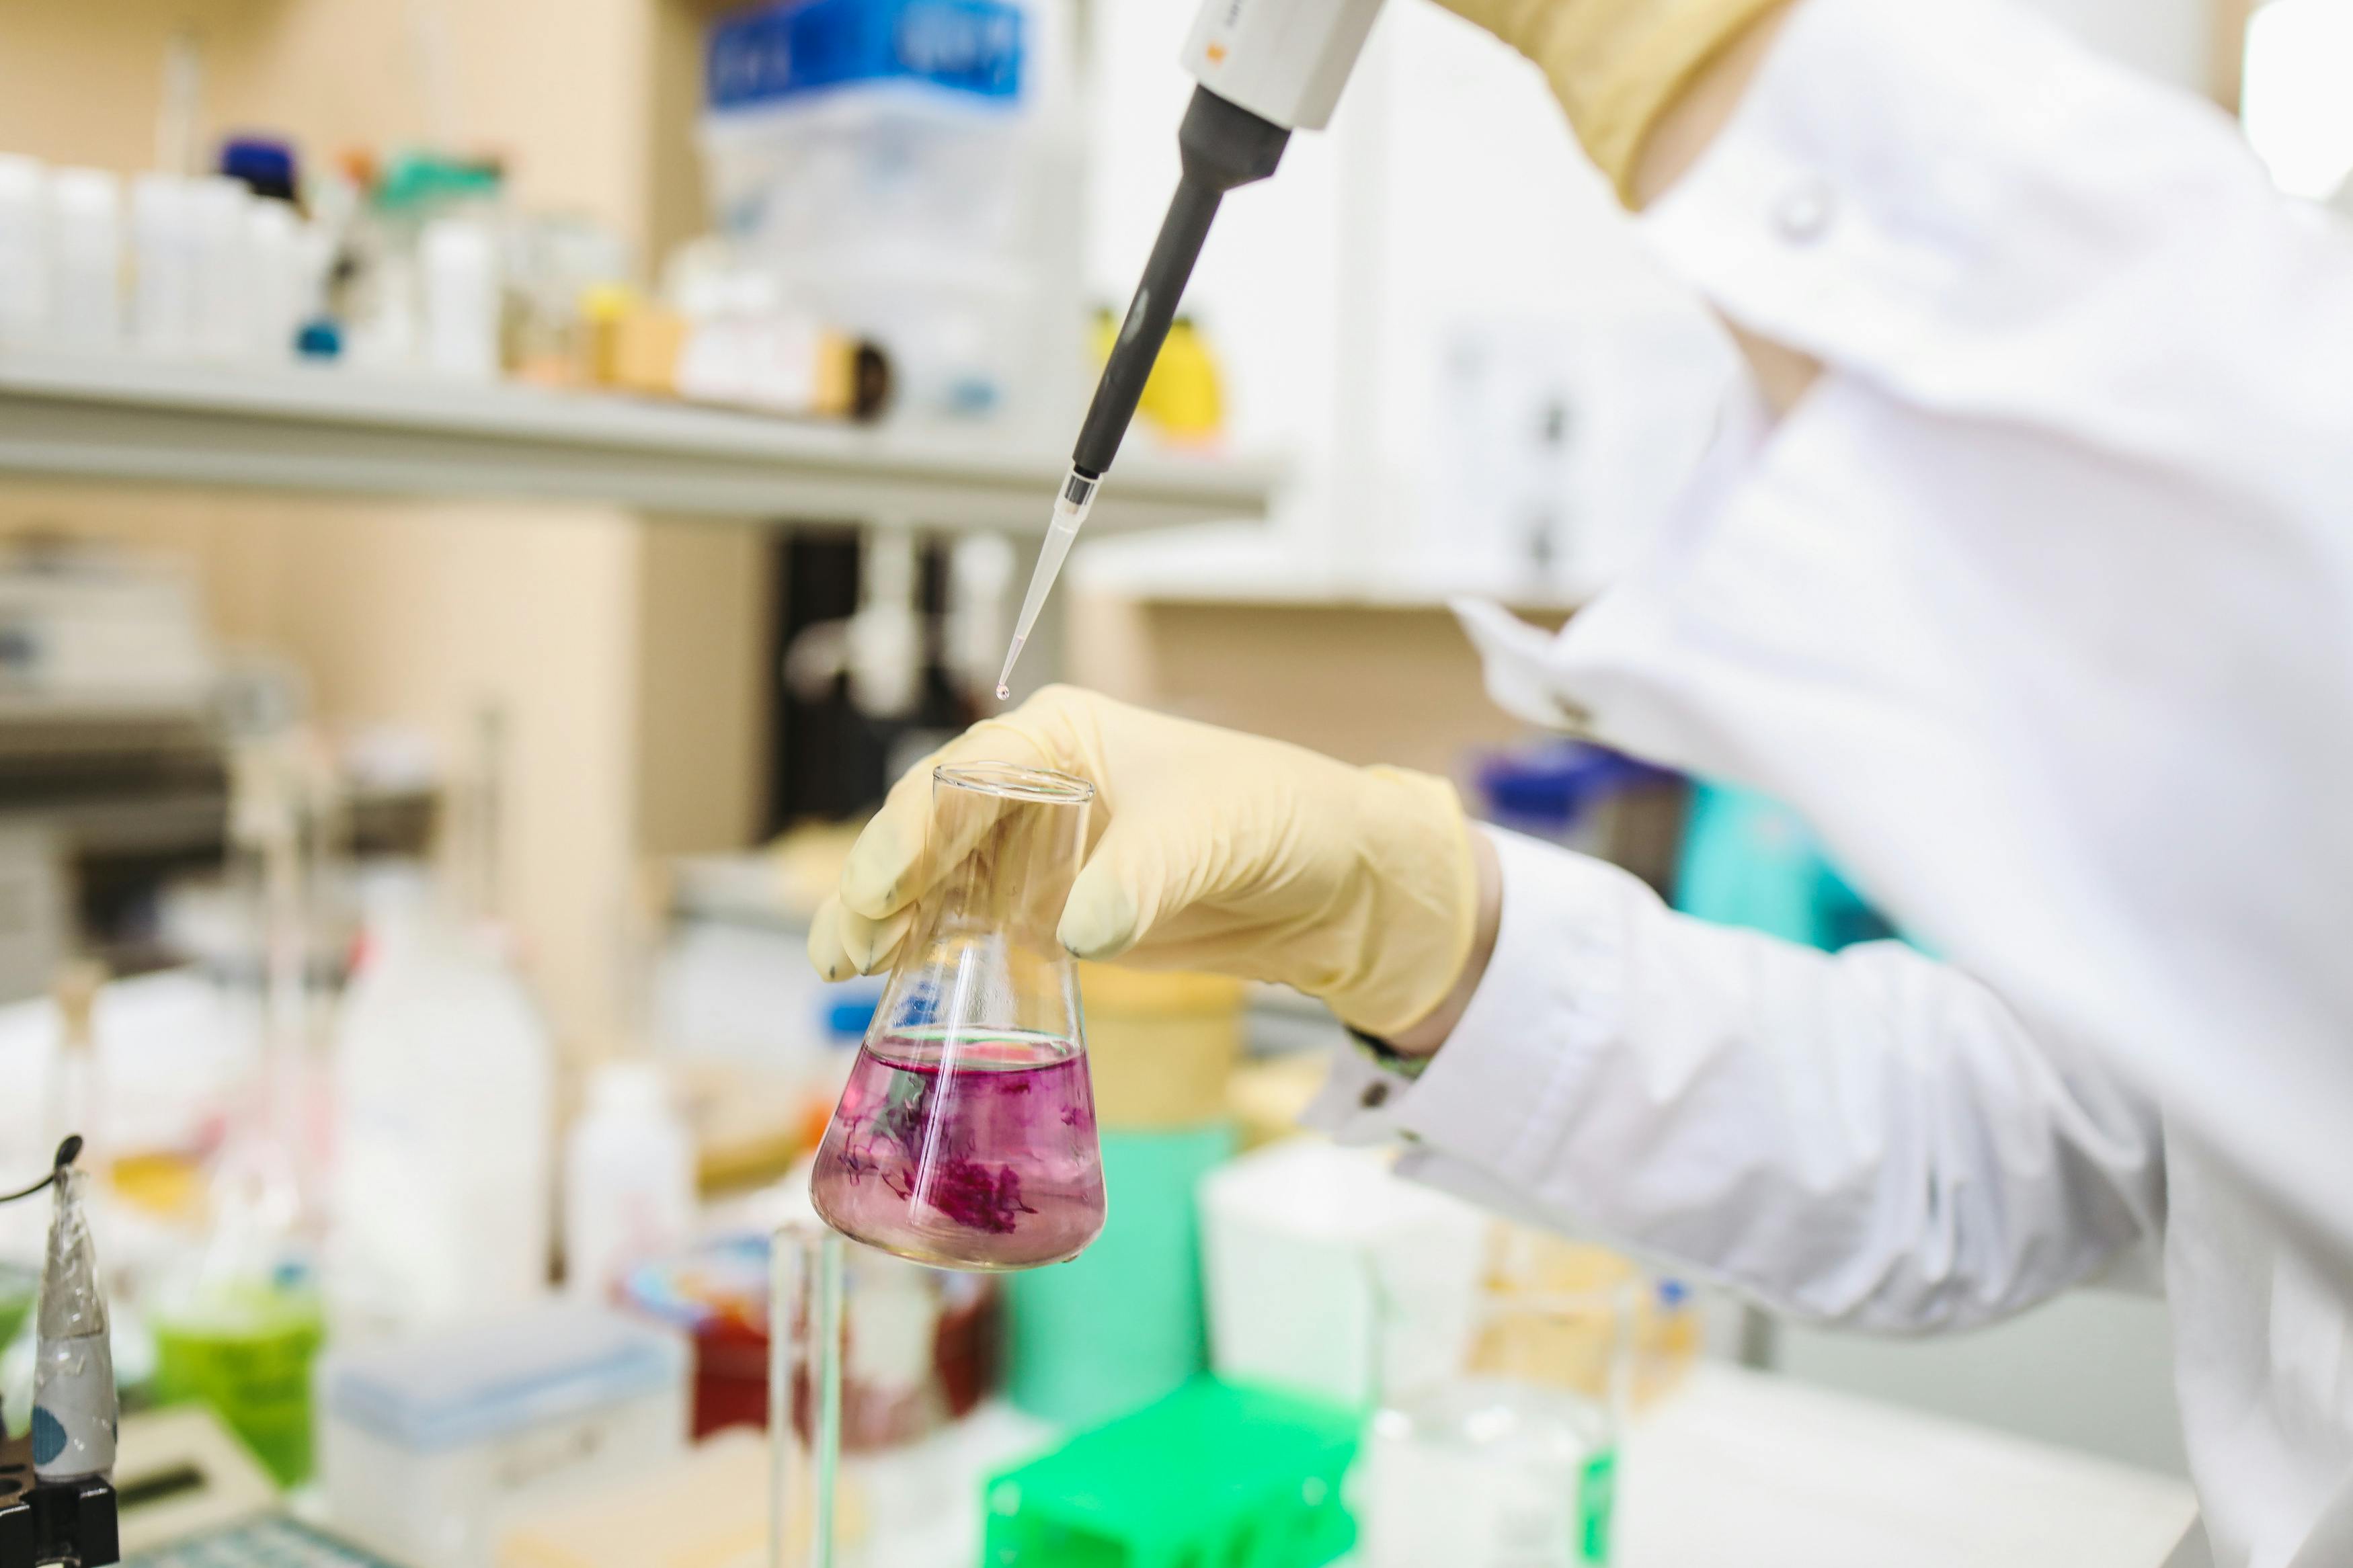
Photo by Polina Tankilevitch on Pexels
Chemical Quality vs. Chemical Purity
Although the terms are closely related, chemical quality and purity are not exactly the same. Purity primarily concerns the amount of the desired chemical and the levels of unwanted substances. Quality is broader and can include purity, identity, consistency, physical characteristics, manufacturing controls, testing, packaging, storage, documentation, and traceability. A chemical with a high purity percentage is not automatically suitable for every pharmaceutical application — manufacturers need to determine whether the complete product specification meets the requirements of the intended process.
Importance of Impurity Control
Impurity control is one of the most important aspects of pharmaceutical raw-material management. Impurities can originate from raw materials, manufacturing processes, reactions, solvents, storage, packaging, cross-contamination, and environmental exposure. Some impurities may have little practical impact at low concentrations, while others may be important even at trace levels depending on their nature and the application.
Effective impurity control helps manufacturers maintain consistent product quality, reduce contamination risks, support formulation stability, improve analytical reliability, meet established specifications, and reduce manufacturing variability. For sensitive pharmaceutical processes, understanding the impurity profile can therefore be as important as knowing the stated assay — a point explored further in our overview of how chemical grades matter in pharmaceutical applications.
Role of Chemical Grades in Pharmaceuticals
Different chemical grades are designed for different applications, and pharmaceutical manufacturers and laboratories may encounter several of them in the same facility. Compendial grades such as USP and NF are defined by United States Pharmacopeia monographs, while laboratory and analytical grades follow different specification systems.
| Chemical Grade | Typical Application | Key Consideration |
|---|---|---|
| Technical Grade | Non-critical industrial applications | General performance |
| Laboratory Grade | Routine laboratory work | Suitable for general testing |
| Reagent Grade | Research and laboratory applications | Controlled quality |
| Analytical Grade | Analytical testing | Defined impurity specifications |
| USP/NF Grade | Applicable pharmaceutical uses | Compendial requirements |
| HPLC Grade | Chromatographic analysis | Low analytical interference |
| Specialty Grade | Specific manufacturing applications | Application-specific specifications |
The appropriate grade should be determined by the specific manufacturing process, analytical method, regulatory requirements, and product specification. For laboratory-focused guidance, see our article on choosing the right chemical grade for lab applications.
How Chemical Quality Affects Pharmaceutical Production
1. Raw Material Qualification
Before a chemical enters production, manufacturers generally need to establish that it meets the required specifications. Consistent raw materials make it easier to maintain predictable manufacturing processes.
2. Formulation Consistency
The quality of ingredients can affect the physical and chemical characteristics of a pharmaceutical formulation. Variations in raw materials may influence solubility, stability, appearance, texture, reaction behavior, and shelf-life characteristics.
3. Process Performance
Chemicals used during manufacturing reactions or processing steps must perform consistently. Unexpected impurities can potentially alter reaction behavior or introduce unwanted substances into the process.
4. Finished Product Quality
Raw-material quality ultimately contributes to the consistency of the finished pharmaceutical product, so maintaining control over incoming chemicals is an important part of overall pharmaceutical quality management.
Chemical Quality in Pharmaceutical Quality Control
Quality control laboratories rely heavily on chemical reagents and reference materials to test raw materials, intermediates, and finished products. The quality of laboratory chemicals can affect accuracy, precision, repeatability, detection limits, analytical sensitivity, and test reproducibility. An unsuitable solvent or reagent may, for example, introduce background interference into an analytical method. For this reason, analytical laboratories should select chemical grades according to the requirements of their validated methods and applicable specifications. Our guide to the essential chemical reagents used in laboratory research covers the main reagent categories in more detail, and the full range is available under lab reagents, biochemicals, and catalysts.
Documentation and Traceability
Quality documentation is an essential part of pharmaceutical chemical procurement. Depending on the product and application, manufacturers may require a Certificate of Analysis (COA), Safety Data Sheet (SDS), product specification, batch or lot number, manufacturing information, storage conditions, regulatory documentation, applicable certificates, and traceability information.
Certificate of Analysis
A Certificate of Analysis provides quality information for a specific batch of material. Manufacturers can use the COA to compare the supplied material against established specifications and support incoming-material verification. FDA guidance on CGMP production and process controls discusses the conditions under which a supplier’s certificate of analysis may be relied upon.
Lot Traceability
Lot traceability helps manufacturers identify the source and batch of a chemical used in production. This can be valuable when investigating quality deviations, batch problems, customer complaints, raw-material variations, and supply-chain issues. Strong traceability also supports effective quality management, and is typically underpinned by a formal quality system such as ISO 9001:2015 certification.
Benefits of High-Quality Pharmaceutical Chemicals
Using appropriately specified, consistent chemicals can provide several practical benefits across production and the laboratory.
| Benefit | What It Supports |
|---|---|
| Better Batch Consistency | More predictable production from batch to batch |
| Improved Process Control | Fewer unexpected changes during manufacturing |
| Reduced Contamination Risk | Controlled impurity profiles |
| Improved Analytical Reliability | Less potential for analytical interference |
| Better Regulatory Readiness | Documentation and traceability for quality activities |
| Reduced Manufacturing Waste | Fewer failed batches, repeat tests, and material losses |
| Improved Supply Chain Management | Consistent specifications and predictable availability |
Risks of Using Low-Quality Chemicals
Selecting chemicals based only on price can introduce additional manufacturing risks. Changes in purity or impurity profiles can contribute to batch-to-batch variation, and uncontrolled impurities may enter pharmaceutical manufacturing processes. Impurities in laboratory reagents can interfere with analytical testing and potentially affect results, while certain impurities can influence chemical or physical stability depending on the formulation. Unexpected raw-material problems can also result in investigations, retesting, or manufacturing interruptions, and materials that do not meet required specifications may create difficulties during quality reviews, audits, or inspections.
How to Choose the Right Chemical Supplier
A pharmaceutical chemical supplier should be evaluated on more than price and availability. Manufacturers should consider the supplier’s ability to provide consistent quality, complete documentation, technical information, and dependable supply.
| Evaluation Criteria | Why It Matters |
|---|---|
| Chemical Purity | Supports consistent manufacturing |
| Impurity Profile | Helps evaluate suitability |
| Product Grade | Matches chemical to application |
| Certificate of Analysis | Provides batch-specific information |
| Safety Data Sheet | Supports safe handling |
| Lot Traceability | Supports quality investigations |
| Regulatory Documentation | Helps meet applicable requirements |
| Consistent Supply | Reduces production interruptions |
| Technical Support | Helps with product selection |
| Packaging & Storage | Protects material quality |
A supplier experienced in pharmaceutical and nutraceutical chemicals can also help customers identify appropriate product grades and specifications. You can browse the full Allan Chemical product range by industry and application.
Future Trends in Pharmaceutical Chemical Quality
The pharmaceutical industry continues to place greater emphasis on raw-material quality, impurity control, traceability, and supply-chain reliability. Advanced analytical techniques are allowing manufacturers to identify increasingly small concentrations of impurities, which increases the importance of carefully controlled chemical specifications. Pharmaceutical companies are also evaluating suppliers more closely on quality systems, consistency, documentation, and supply reliability, and are increasingly matching chemical grades to specific manufacturing and analytical requirements rather than using general-purpose chemicals for every process. Digital quality systems and supply-chain technologies are helping manufacturers maintain better visibility of raw materials, batches, documentation, and supplier information, while reliable availability of critical pharmaceutical chemicals is becoming more important as manufacturers seek to minimize production interruptions.
Sourcing chemicals for pharmaceutical production?
Allan Chemical supplies USP, NF, ACS, and other specialty grade chemicals in original sealed manufacturer containers, with a Certificate of Analysis and SDS included on every shipment.
View Specialty Chemicals at Allan ChemicalContact our team | Or call (973) 962-4014 | info@allanchem.com
FAQs
Why is chemical purity important in pharmaceutical manufacturing?
Chemical purity helps control unwanted substances that may affect manufacturing processes, formulation characteristics, analytical results, and finished-product quality.
Is higher chemical purity always better?
Not necessarily. The appropriate chemical should meet the specifications required for the intended application. A higher-purity grade may not provide additional value when it exceeds the actual process requirements.
What is the difference between chemical purity and chemical quality?
Purity primarily describes the amount of the desired chemical and its impurities. Quality is broader and can include purity, identity, consistency, physical characteristics, documentation, packaging, storage, testing, and traceability.
Why are impurity profiles important?
Different impurities can have different effects. Understanding their identity and concentration helps manufacturers determine whether a chemical is appropriate for a specific pharmaceutical application.
What chemical grades are used in pharmaceutical applications?
Depending on the application, pharmaceutical operations may use laboratory, reagent, analytical, USP/NF, HPLC, and other specialized grades.
What is a Certificate of Analysis?
A Certificate of Analysis is a document that provides quality and test information for a specific batch of a chemical product.
How does chemical quality affect pharmaceutical quality control?
The quality of laboratory reagents and other testing materials can influence analytical accuracy, precision, repeatability, and potential interference.
What should pharmaceutical manufacturers look for in a chemical supplier?
Important considerations include product quality, specifications, impurity control, documentation, lot traceability, reliable supply, technical support, and experience with pharmaceutical applications.
References
- USP — USP–NF Compendial Standards for Drug Substances and Excipients
- ICH — Quality Guidelines (including impurity guidelines Q3A/Q3C/Q3D)
- U.S. FDA — Current Good Manufacturing Practice (CGMP) Regulations
- American Chemical Society — ACS Reagent Chemicals: Specifications and Procedures
This article is for general information and is not regulatory, safety, or formulation advice. Always consult the current official regulations and qualified professionals for your specific application.


Comments are closed